
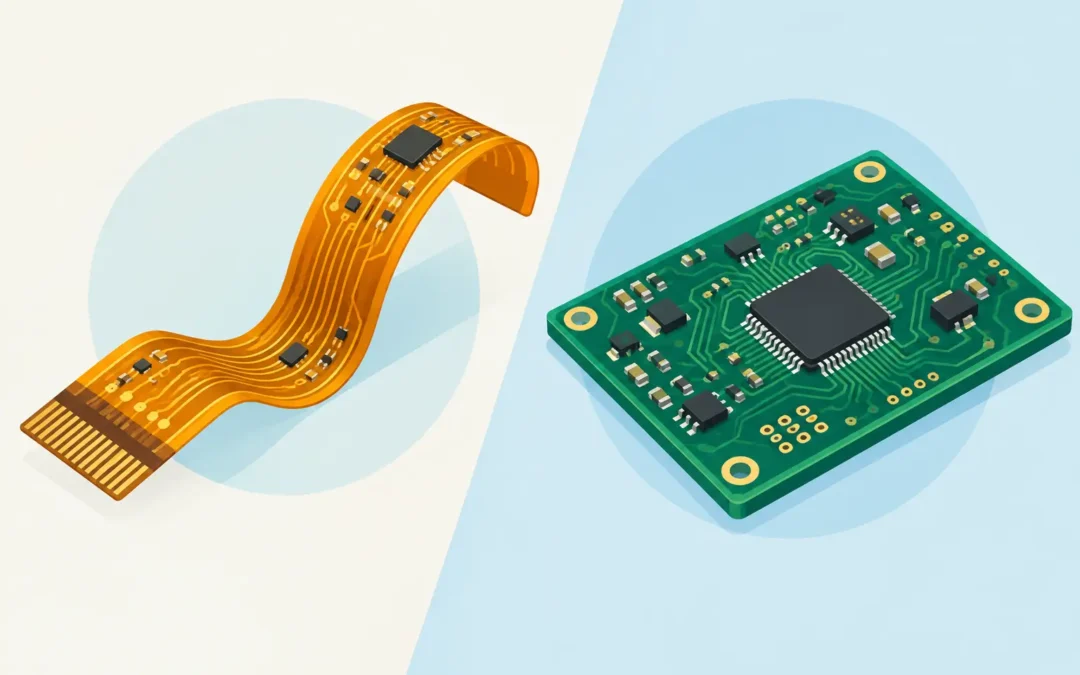
A board that fits comfortably on a bench can become the wrong architecture once it must survive vibration, fit a moving mechanism, or install inside a tightly packaged enclosure. The flex versus rigid PCB decision is therefore not simply a materials choice. It affects mechanical packaging, interconnect reliability, assembly flow, test strategy, recurring cost, and the long-term serviceability of the finished product.
Rigid boards remain the right answer for many electronics programs. Flexible circuits solve problems that a flat, fixed board cannot. Between them is rigid-flex, which can place components on rigid sections while using integrated flex sections to carry signals through bends and between planes. The most effective choice starts with the actual mechanical and electrical job the circuit must perform.
Flex Versus Rigid PCB: The Core Difference
A rigid PCB is built on a stiff substrate, commonly FR-4, that holds its shape throughout manufacturing and use. It offers a stable platform for component placement, automated assembly, connectors, heat-generating devices, and fixture-based testing. For designs that remain flat and stationary inside a product, this mechanical stability is often an advantage.
A flex circuit uses thin polyimide-based dielectric materials and rolled or electrodeposited copper to create a circuit that can bend, fold, or move. It may be designed for a one-time installation fold, repeated dynamic flexing, or a compact three-dimensional routing path. Flex circuits are not simply rigid boards made thinner. Their material stackup, copper selection, coverlay, stiffeners, bend geometry, and termination design must be engineered around the application.
Rigid-flex combines these constructions in a single integrated circuit. The rigid areas support components and provide mounting surfaces, while flexible tails or interconnect sections eliminate discrete wiring and board-to-board connectors. In regulated and high-reliability equipment, the value is often fewer interconnect points, controlled documentation, and a more repeatable installation.
When a Rigid PCB Is the Better Engineering Choice
Choose a rigid PCB when the circuit needs to be structurally self-supporting and the enclosure does not demand folding or movement. Rigid boards are typically easier to panelize, process through standard assembly lines, inspect, rework, and test with conventional fixtures. They also provide straightforward support for heavier components, large connectors, heat sinks, and high-pin-count devices.
Cost can favor rigid construction when the product has adequate space and requires no cable replacement or dimensional reduction. A simple, low-layer-count rigid board generally uses familiar materials and a broad manufacturing process. For high-volume products with a static layout, that can produce an efficient and economical solution.
Rigid construction also deserves close consideration where thermal management drives the design. Copper weight, metal-core options, thermal vias, and contact with a chassis can all be incorporated into a rigid solution. Flex can carry power and can include thermal features, but a thin flexible section should not be expected to solve a heat problem created by component density.
That said, a rigid board paired with wire harnesses or multiple connectors should be evaluated as a complete system. The bare board may be less expensive, yet the finished assembly can accumulate cost through connector procurement, hand assembly, routing labor, inspection, and field failures at interconnect points.
Where Flexible Circuits Earn Their Place
Flex is most valuable when it replaces a separate cable, supports compact packaging, or allows an electronic assembly to conform to the shape of the product. A flexible circuit can fold around a housing, pass through a hinge, route through a narrow channel, or connect modules that sit on different planes. These capabilities are especially useful in avionics, medical devices, automotive systems, industrial robotics, and compact consumer equipment.
The reliability benefit often comes from part-count reduction. Replacing wire bundles, connector pairs, and manually routed interconnects with one formed flex circuit can reduce opportunities for incorrect installation and intermittent contact. In vibration-sensitive equipment, fewer mated connections can also mean fewer potential failure locations.
Weight and volume are meaningful factors in aerospace, defense, and portable equipment. A thin flex circuit can reduce both, particularly when it consolidates multiple point-to-point connections into a single patterned interconnect. The gain is not automatic, however. Stiffeners, shielding, connectors, and protective layers add material, so the complete assembly should be compared rather than only the circuit outline.
Dynamic applications require more discipline than static folds. If a flex circuit will move repeatedly, the design must define bend radius, flex life expectations, cable path, strain relief, copper type, and the location of vias, pads, and layer transitions. A circuit intended to fold once during installation can use different construction rules than one operating through millions of cycles in a robotic joint or printer mechanism.
Design Rules That Matter in Flex
Several flex design details have an outsized effect on manufacturing yield and field performance. Traces should generally run perpendicular to the bend line rather than parallel to it, and pads or vias should be kept out of the bend area whenever possible. Transitions from rigid to flex areas need controlled geometry and strain relief. Sharp corners, abrupt trace-width changes, and unsupported terminations concentrate stress.
Stiffeners provide localized support beneath connectors, surface-mount components, and insertion areas. They do not make a flex circuit equivalent to a rigid board, but they can create the stability required for assembly and handling. Coverlay and bonded cover materials protect conductors while preserving controlled flexibility, whereas solder mask is more commonly associated with rigid-board processing.
Electrical requirements still apply. Controlled impedance, shielding, fine trace and space, high-density interconnects, and multilayer routing can all be incorporated into flex and rigid-flex designs. The trade-off is that each added requirement interacts with material selection and process capability. Early discussion between the design team and manufacturer prevents a drawing from specifying a geometry that is technically possible but unnecessarily difficult to build consistently.
Rigid-Flex for Integrated, High-Reliability Assemblies
Rigid-flex is often selected when a design team needs the component support of rigid boards but wants to eliminate cable assemblies between them. Rather than joining separate boards with connectors and harnesses, rigid-flex integrates the interconnect into the circuit itself. This can simplify final installation and improve packaging control in three-dimensional assemblies.
The value is strongest when the product architecture is stable enough to justify a tailored construction. Rigid-flex requires more up-front coordination than a standard rigid board because layer stackups, flex exposure areas, bend locations, lamination sequence, and assembly access must work together. Changes late in the design cycle can be more consequential.
For mission-critical programs, the added engineering effort can be justified by fewer parts to qualify and fewer interfaces to manage. It can also improve traceability when fabrication and assembly are controlled by one accountable domestic supplier. GC Aero Flexible Circuits supports these requirements from prototype through production with in-house flex fabrication and integrated assembly capability.
Compare the Total Cost, Not the Board Price
The wrong comparison treats a flex circuit and a rigid board as interchangeable line items. A more useful analysis includes the full installed system: circuit fabrication, connectors, wire harnesses, assembly labor, test fixtures, inspection, packaging constraints, failure risk, and expected field service.
Flex may carry a higher unit price than a simple rigid board, especially at low quantities or with multilayer construction. Yet it may remove several purchased connectors and substantial manual assembly. Conversely, specifying flex for a stationary, spacious product with no interconnect problem can introduce cost and design complexity without a measurable return.
Prototype quantities also deserve their own decision path. Early builds may use a practical rigid-board approach to validate electronics, while the production package is developed as flex or rigid-flex once enclosure dimensions, cable paths, and installation procedures are confirmed. This approach can be sensible, provided the program recognizes that moving to flex later is an engineering transition, not a file conversion.
Questions to Resolve Before Releasing the Design
Before selecting the construction, determine whether the circuit must bend once, bend repeatedly, or remain fixed. Define available routing space, component mass, connector locations, environmental exposure, vibration levels, shielding needs, thermal paths, and service access. For aerospace and defense work, include traceability, export-control requirements, inspection documentation, and supply-chain location from the start.
Then ask a practical question: is the circuit merely carrying signals between fixed boards, or is it part of the product’s mechanical architecture? If it must fold, move, reduce connector count, or occupy a path that no rigid board can reach, flex or rigid-flex should be evaluated early. If it needs a stable, economical component platform and the package allows it, rigid may remain the better choice.
The best circuit architecture is the one that makes the finished product easier to build, test, install, and support for the life of the program. Bringing the fabricator into that decision before mechanical constraints harden gives the team more options and fewer expensive surprises.
For more on this topic, see: how to specify flex circuitry.
For more on this topic, see: FPC shielding design.